Choosing a Pcb X Ray Machine is not simply a matter of comparing prices. The right system depends on the parts being inspected, the defects that matter, and the pace of production. A compact board with dense components may need different imaging performance from a large assembly. Small details matter.
China has a broad manufacturing base for industrial X-ray equipment, but suppliers differ in design, applications, and after-sales support. This guide introduces ten manufacturers associated with the Chinese market and offers practical points for comparing them. It considers factors such as X-ray source specifications, detector resolution, image software, sample capacity, operator training, and service access. These details can shape daily use as much as the headline specification.
The “Top 10” label should be treated as a shortlist, not a universal ranking. A strong fit for one factory may not suit another. Before requesting a quotation, define the inspection task and ask for sample imaging, technical documentation, and clear warranty terms. Check whether stated capabilities match your own parts and workflow. A polished demonstration is useful, but it may not answer every question. Sometimes the evidence is incomplete. That deserves a closer look. Manufacturer information can change, so verify current models, certifications, and service arrangements directly with each supplier.
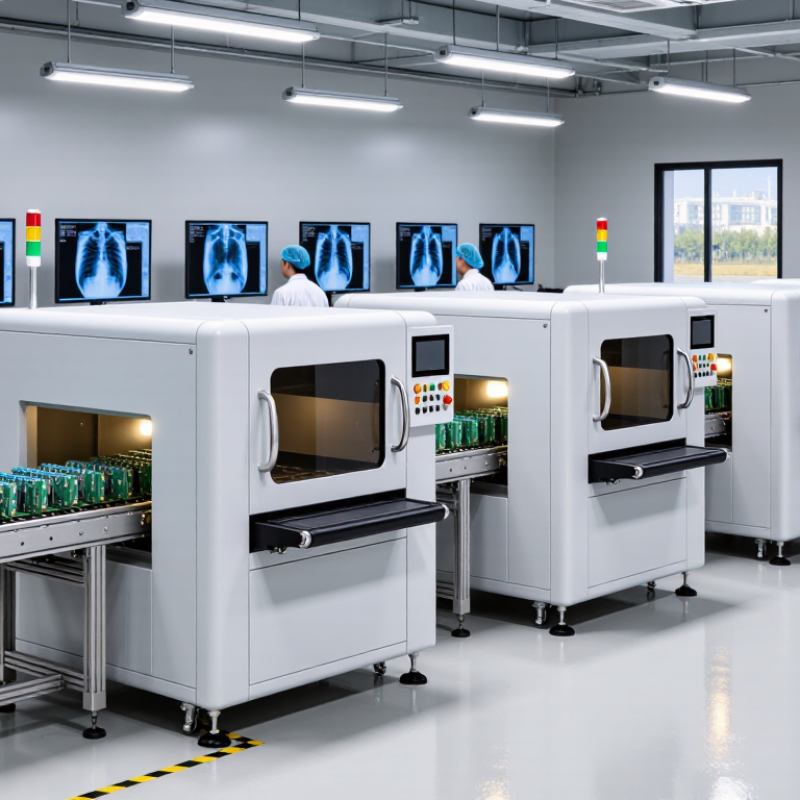
X-ray inspection reveals solder joints hidden beneath BGA packages, where visual checks cannot reach. In 2D imaging, one beam produces a flat projection. It can quickly show missing solder, bridging, and uneven ball shapes. But overlapping features may hide a defect. A dark spot is not automatically a void. Board thickness, component geometry, and image settings all affect interpretation.
For complex assemblies, 3D computed tomography captures images from multiple angles and reconstructs slices through the joint. The National Physical Laboratory’s Good Practice Guide 145 explains how voxel size and measurement uncertainty affect industrial CT results. Finer detail helps, but it does not guarantee a correct diagnosis. Operators still need suitable contrast, calibration, and repeatable inspection settings. IPC-7095D also outlines BGA assembly and inspection considerations, including voiding and joint quality.
Scale makes reliable inspection important. Grand View Research estimated the global PCB market at about USD 76.4 billion in 2023, reflecting the breadth of products built on these boards. That figure is not an inspection-performance measure. For BGA analysis, teams should compare images with acceptance criteria and review suspicious joints from more than one angle. Even experienced inspectors can mistake harmless structure for a defect. A second review is sometimes worthwhile.
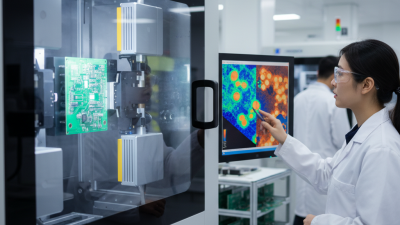
A microfocus spot size of 1–5 μm can help reveal small solder voids, hairline cracks, and hidden joint defects in dense PCB assemblies. But spot size is not the same as image resolution. Resolution also depends on detector pixel pitch, magnification, geometry, exposure, and vibration. A nominal 1 μm source may therefore produce no finer detail if the detector or setup becomes the limiting factor. Small numbers look impressive. Verify them in images.
For comparable evaluations, ask manufacturers for measured basic spatial resolution, not only a focal-spot specification. ASTM E2002 describes methods for determining image unsharpness and basic spatial resolution in radiography and radioscopy. ISO 19232-5 specifies duplex-wire image-quality indicators for assessing that resolution. Request test images made at your working magnification, with representative PCB materials and thicknesses. Check whether tiny void edges remain distinct, not merely visible. Also compare repeatability across several scans. In practice, this part is often underreported. A clear image from one carefully tuned sample does not prove stable performance on a production line. Include detector pixel size, source-to-object distance, and exposure conditions in the comparison record.
When comparing China’s top 10 PCB X-ray machine manufacturers, start with the boards you actually inspect. A dense multilayer board needs different imaging performance from a simple single-sided PCB. Check stated resolution, magnification range, inspection area, and whether the machine handles your largest panel. Ask each supplier to scan the same sample board. Useful details show up in the image, not just the specification sheet. Small vias matter.
Look closely at repeatability and workflow. Can operators save inspection recipes, mark suspected voids, and export clear images for review? Ask for a live demonstration using boards with known defects, such as a partially filled via or a misaligned component. Note scan time and how much manual adjustment is required. A polished demonstration can hide setup effort. Request operating data from a comparable production environment, if available.
Service deserves equal attention. Confirm installation support, operator training, spare-part availability, and typical response times. Ask who handles software updates and whether remote diagnostics are available. Also inspect the enclosure, door interlocks, and radiation-safety documentation; request records rather than relying on verbal assurances. Compare total ownership costs, including maintenance and training, not only purchase price. I would still verify every claim independently. That takes time, but it can prevent an expensive mismatch.
Suggested buyer-defined weighting for comparing PCB X-ray inspection systems. These percentages are an evaluation framework, not measured scores or rankings of manufacturers.
Use the same criteria and test samples for every supplier. Adjust the weights to match your inspection needs, then assess each manufacturer using documented specifications, sample results, and service terms.
In PCB production, X-ray inspection reveals defects hidden beneath packages and solder masks. For buyers comparing China’s top ten PCB X-ray machine manufacturers, practical performance matters more than a bright image. A system should show repeatable detail across different board sizes, component heights, and inspection angles. Small, clear steps matter.
Voids in solder joints can weaken thermal transfer and reduce mechanical reliability. X-ray images help assess void size, shape, and position, but results depend on resolution, contrast, and sample setup. A single dark area does not prove a process failure. Compare similar joints, use consistent settings, and confirm findings against suitable acceptance criteria. Tiny voids can be difficult to distinguish from overlapping copper features. Not always obvious.
For solder-joint inspection, angled views can reveal insufficient fill, bridging, or uneven ball collapse beneath hidden packages. Component checks may identify missing parts, misalignment, polarity issues, or internal damage. Operators should review image-quality controls and verify calibration with known references. A clean image can still mislead. Board layout, material density, and viewing angle all affect what appears visible, so experienced teams may interpret the same image differently. X-ray inspection is useful, but it cannot replace process data or careful judgment.
When comparing China’s top PCB X-ray machine manufacturers, treat throughput as a production measure, not a brochure number. Ask how many boards the system inspects per hour at your actual board size and inspection settings. A line handling dense multilayer boards may need slower, more detailed scans than a line checking simple assemblies. Numbers can mislead. Request a trial using representative boards, including samples with small voids or hidden solder defects.
Automation should fit your workflow. Check how boards load, how results reach your traceability system, and what happens when a scan flags a defect. Safety features should include clear status indicators, interlocks, and documented operating procedures; ask to see them during a demonstration. After-sales support matters when production stops. Confirm response hours, spare-parts availability, remote troubleshooting, and training scope. A polished demo is not a production shift, and support promises can sound vague. Get service terms and acceptance criteria in writing, then review them with the people who will run the machine.