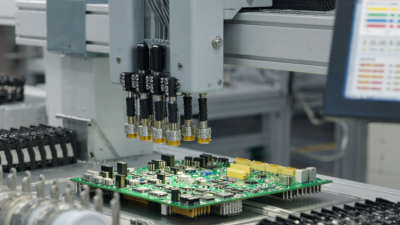
Buying an Smt Machine is not just a matter of comparing placement speeds. The right choice must fit your products, factory conditions, staffing, and plans for future growth. For global buyers, the details matter: feeder availability, software support, local service, and the time required to change a production line.
Demand signals make careful planning more important. In its Spring 2024 forecast, the World Semiconductor Trade Statistics organization projected global semiconductor sales of $611.2 billion in 2024, up 16 percent from 2023. Semiconductor sales are not a direct measure of SMT equipment demand. Still, they show how quickly production needs can shift. IPC’s electronics manufacturing resources also highlight the importance of process capability and quality across the supply chain. A machine’s headline placement rate alone cannot tell you whether it will meet those needs.
Look beyond the brochure. Compare placement accuracy, supported component sizes, board dimensions, feeder capacity, and actual changeover procedures. Ask suppliers to demonstrate a representative job, including inspection and recovery from a placement error. Check spare-parts lead times and technician coverage in your region. A low purchase price can become expensive if a line waits days for a critical feeder or software fix. And some specifications still need questioning. “Maximum speed” may describe ideal conditions, not your mixed-product shift. This guide offers ten practical buying tips to help global buyers assess the full picture, ask better questions, and choose equipment with fewer costly surprises.
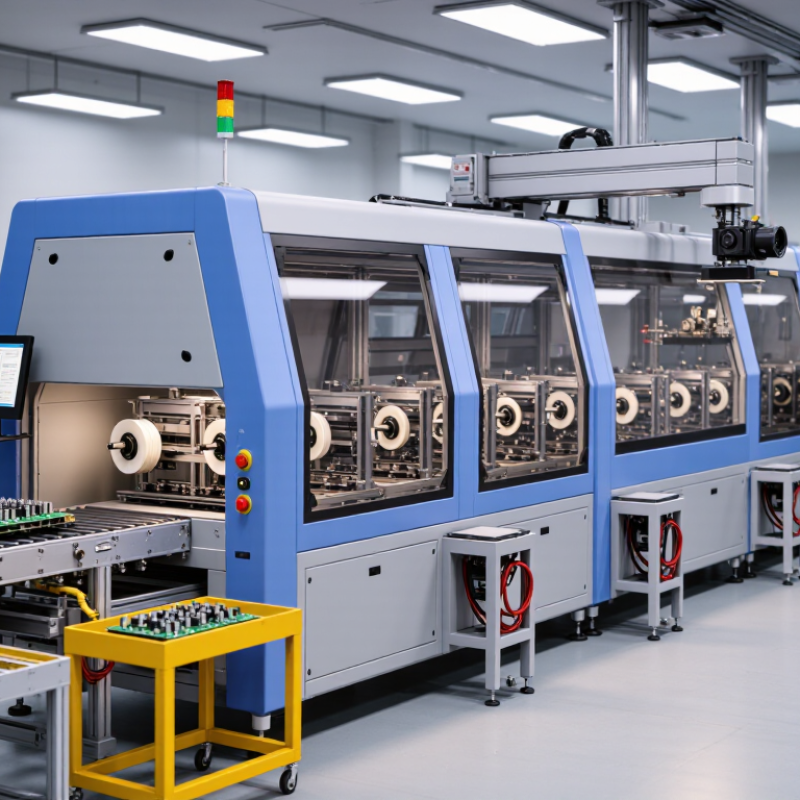
Before comparing SMT machines, define what the line must build each day. List product types, board dimensions, component packages, and the expected mix of low- and high-volume orders. Include difficult parts, such as fine-pitch components or tall connectors, because they can affect placement accuracy and feeder setup.
Estimate output from actual demand, not the machine’s advertised placement rate. For example, calculate boards per shift using the slowest process, then allow time for changeovers, replenishment, inspection, and planned maintenance. A line targeting 600 boards per shift may need more capacity if it switches products several times daily. Reality is messier. Keep a modest buffer, but avoid buying capacity that your workforce or upstream processes cannot support.
Ask suppliers to model your real production data, including representative board files and component lists. Confirm the assumptions behind cycle-time estimates, especially nozzle changes, board handling, and inspection pauses. Run a trial when possible, and record usable output across a full shift rather than relying on a short demonstration. The estimate may still be imperfect; actual yield and operator experience can change the result. Be prepared to revise it.
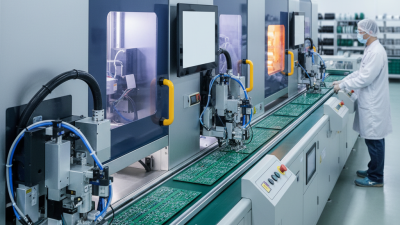
Use this planning checklist to describe your production needs before comparing equipment. The figures below are illustrative planning inputs, not guaranteed machine performance; validate capacity using your own boards, components, process settings, and operating schedule.
| No. | Requirement to Define | Example Input or Measure | Why It Matters When Buying |
|---|---|---|---|
| 1 | Monthly board demand | Plan for 20,000 good boards per month, separated by product type and expected demand variation. | The machine and line should be sized for required good output, rather than an isolated peak-speed figure. |
| 2 | Board dimensions and panelization | Record each board’s length and width, thickness, weight, panel arrangement, and any edge-clearance or support needs. | Board size and handling requirements affect conveyor compatibility, support configuration, and whether panels can run reliably. |
| 3 | Product mix and volume by model | List annual and monthly quantities for each board model, including low-volume variants and planned new products. | A high-mix operation may need faster changeovers and flexible feeder capacity, while a stable high-volume mix may prioritize sustained throughput. |
| 4 | Placements per board | For planning, a board with 1,200 component placements produced at 20,000 boards per month requires 24 million placements per month. | Placement demand is a more useful starting point than a machine’s headline placements-per-hour rating; actual output also depends on component mix and board layout. |
| 5 | Component and package mix | Count component types and feeder positions; identify fine-pitch, small-chip, large, odd-form, and polarity-sensitive parts. | Different component sizes, pickup methods, and placement requirements can affect attainable speed, accuracy, tooling, and feeder configuration. |
| 6 | Working calendar and shifts | Example schedule: two 8-hour shifts per day, 22 production days per month, or 352 scheduled hours per month before breaks and losses. | Available production time determines the output rate the line must sustain. Clarify whether shift hours include breaks, maintenance, and planned changeovers. |
| 7 | Changeover frequency | Estimate model changes per shift and record the time needed to change feeders, programs, stencils, and board supports. | Frequent changeovers reduce production time. Compare the complete changeover process and required feeder setup, not just the machine cycle time. |
| 8 | Good-output and availability assumptions | For an initial planning scenario, applying a 70% effective production factor to 352 scheduled hours gives about 246 effective hours per month. | A planning factor can account for stops, setup, and other losses, but actual performance varies. Use factory data or a production trial to establish realistic assumptions. |
| 9 | Required net production rate | At 20,000 boards over 246 effective hours, the average required output is about 81 boards per effective hour, or one board every 44 seconds. | Translate monthly demand into a net rate, then check whether the proposed line can meet it with your actual program, component mix, and process route. |
| 10 | Capacity margin and acceptance test | Set a documented capacity margin above the calculated requirement, then test representative boards and components using agreed output, quality, and changeover criteria. | A production-based acceptance test helps confirm usable capacity and quality under defined conditions. Agree in advance on measurement methods, test duration, and pass criteria. |
SMT equipment should be compared as a connected production line, not as isolated machines. A stencil printer applies solder paste, a pick-and-place machine positions components, and a reflow oven forms solder joints. Their roles differ, so compare cycle times only after checking how boards move between them. A fast placer may still wait behind a slower printer. Small details matter.
Match each machine to the actual board mix. Check minimum and maximum board dimensions, component sizes, feeder capacity, and changeover time. A line handling tiny passives and fine-pitch parts may need different placement accuracy than one building larger, simpler assemblies. Ask how programs are created and transferred, too. Compatible data formats can reduce setup work, but confirm this with a sample job before purchase. Paper compatibility is not always shop-floor compatibility.
Utilities and layout deserve equal attention. Measure the available floor space, power supply, compressed air, extraction needs, and service access. Leave room to open covers and load feeders without blocking nearby operators. Buyers sometimes focus on headline speed and overlook these constraints; that looks efficient on a spreadsheet, then feels awkward during installation. No configuration is perfect. Compare options against expected volume, product changes, and operator skills, and record which assumptions still need testing.
When evaluating an SMT machine supplier, look beyond the sales presentation. Ask how long common wear parts take to ship and whether engineers can support installation, calibration, and operator training. Request references from customers with similar production volumes and product changes. A useful reference can explain how quickly a real issue was resolved, not just how well the machine ran on delivery. That matters.
Tip: Ask the supplier to provide a written support plan. Check service hours, response targets, spare-parts availability, and escalation contacts. Confirm who pays for travel or remote troubleshooting. Get the details before comparing quotes.
Global support should fit your site’s working hours and communication needs. A time-zone gap can turn a minor feeder fault into a full shift of lost output. Check whether technical documents are clear, training can be repeated for new operators, and remote support works with your network policies. Request a sample maintenance guide or troubleshooting checklist. Small details count. A polished demo can still leave gaps; I would not assume every promise is operational until it is documented and checked with a customer reference.
An SMT machine’s purchase price rarely reflects its full cost. Build a five-year estimate covering tooling, feeders, software licenses, operator training, installation, and scheduled maintenance. Add expected power use and the cost of compressed air or extraction systems where required. Spare parts matter, too. A worn feeder or delayed replacement board can stop a line and affect delivery schedules. Ask suppliers for maintenance intervals, typical service response times, and a parts list with prices. Compare estimates using the same production volume and shift pattern. Small costs add up. Even a careful spreadsheet can miss local labor rates or shipping delays, so mark assumptions clearly and revisit them before signing.
Compliance needs equal attention. Requirements can vary by destination and installation site, so verify applicable electrical safety, electromagnetic compatibility, machinery safeguarding, and environmental documentation with qualified local advisers. Confirm that the machine’s voltage and frequency match the facility, and check whether guards, emergency stops, labels, and manuals meet local expectations. Request relevant test reports and declarations before shipment, then confirm that model numbers match the delivered equipment. A certificate alone may not prove every installed configuration complies. Paperwork can lag. Keep a written record of what was checked, by whom, and when; this makes gaps easier to spot during installation and acceptance testing.
Before buying an SMT machine, map its route from the receiving dock to the production floor. Measure doorways, ceiling height, floor capacity, and service clearances. A machine may fit on a layout but still fail to pass a narrow turn. Confirm power, compressed air, exhaust, and network requirements with your facility team. Request a site-readiness checklist and written utility specifications. Small details matter. A late cable change can postpone commissioning and disrupt other work. Include installation, calibration, and acceptance testing in the purchase schedule, with clear responsibilities for both teams.
Training should cover daily operation, feeder setup, product changeovers, program checks, and recovery from common placement errors. Ask for hands-on practice using your own board files and components, not only a standard demonstration. Keep instructions available in the language operators use, and record who has completed each task. I would not assume one session is enough; staff turnover and infrequent changeovers can expose gaps later. For maintenance, clarify inspection intervals, recommended spare parts, software support, and expected response times. Track nozzle wear, cleaning, alarms, and service visits in a simple log. It may feel tedious at first, but those records help distinguish a recurring machine issue from a process problem.
Plan installation, training, and long-term maintenance before choosing your equipment.
Example planning cadence: daily, weekly, monthly, and annual activities equate to approximately 365, 52, 12, and 1 occurrences per calendar year. Confirm actual inspection and service intervals with the machine manufacturer’s maintenance manual.